This guide provides a practical B2B decision framework. Final specifications, market obligations, testing scope, labels, packaging and shipment requirements must be confirmed for the exact finished SKU and destination.
2. Direct-answer introduction
A robust LCD writing tablet pre-shipment inspection checklist should convert the approved sample and purchase order into observable pass/fail requirements before goods leave the factory. At minimum, it should identify the production lot, set the sampling plan and acceptance criteria, verify the tablet’s writing, erase, lock, stylus and power functions, assess appearance and assembly, confirm the correct battery configuration and warnings, inspect inner and master cartons, and record a clear shipment-release decision.
The practical goal is not to prove that every unit in a large lot is perfect. It is to obtain evidence that the lot conforms to the agreed specification at the chosen sampling risk, while isolating any safety, functional, cosmetic, packing or traceability issue that would make shipment unsuitable. Acceptance sampling by attributes records whether each sampled unit has a stated characteristic or nonconformity, then compares the count with a predetermined acceptance or non-acceptance criterion. This is the logic used by AQL-based systems such as ISO 2859-1 and ANSI/ASQ Z1.4.1 2
For an LCD writing tablet, “functional” must be defined more precisely than “turns on.” Many common models use a pressure-responsive liquid-crystal writing surface and a battery-powered erase pulse rather than an illuminated, pixel-addressable display. The inspection must therefore test the actual agreed mechanism: legible writing across the active area, a complete erase when unlocked, prevention of erase when locked, secure stylus retention where supplied, and the specified battery or charging behavior. A wireless, rechargeable, backlit or app-connected variant needs additional model-specific checks.
This guide is a buyer-side planning framework, not a declaration that every tablet configuration is regulated or compliant in every market. Market-access requirements depend on the product’s functions, intended user, battery type and destination. A final inspection supports quality control; it does not replace applicable conformity assessment, product testing, documentation, or shipping classification. If you want a model-specific checklist aligned to an approved sample and purchase order, email info@lcdwritingtablet.com.
3. Who this guide is for
This guide is for importers, distributors, brand owners, education suppliers, promotional-product buyers and e-commerce operators placing bulk orders of LCD writing tablets. It is particularly useful when a buyer has selected a size, housing color, packaging language, logo treatment, accessory set or battery configuration and now needs to decide what “acceptable production” means before the balance is paid or freight is booked.
It also applies to procurement and quality teams that use a Shenzhen OEM/ODM supplier but employ either the supplier’s quality staff or an independent inspector. The checklist should be owned by the buyer: the factory can execute it, but the buyer must approve the product specification, defect definitions, sampling basis and disposition authority. A third-party inspector cannot infer requirements that were never written down.
The framework assumes a finished consumer tablet that is substantially produced, packed and ready for shipment. It is not a substitute for incoming-component control, process audits, laboratory reliability testing or a factory audit. Those controls happen at different stages and answer different questions. A pre-shipment inspection is most valuable when it confirms that the packed lot matches a stable, approved reference and identifies issues while rework, sorting or carton replacement is still possible.
For products intended primarily for children aged 12 or younger in the United States, the importer or domestic manufacturer should separately determine applicable children’s-product rules. CPSC states that covered children’s products require third-party testing and a Children’s Product Certificate based on results from a CPSC-accepted laboratory.8 A production inspection report is useful supporting evidence, but it is not that certificate.
4. Buyer decision framework
Freeze the reference before production finishes
The inspection starts with a golden sample or signed approved sample. Photograph it from all sides and identify its model number, screen size, color, material finish, stylus type, lock control, battery type, packaging revision and accessories. Attach the approved artwork, dielines, barcode file, user instructions, carton markings and purchase order. A supplier’s catalog image is not a sufficient inspection standard because it rarely captures exact colors, logo placement, accessory fit or language.
Translate each requirement into a simple instruction: what is checked, how it is checked, which sample units are checked, and what passes. For example, “erase works” is ambiguous. “With lock off, write five continuous strokes in the center and at four defined areas; press erase once; no intentional writing remains visible under normal viewing conditions” is inspectable. “No scratch” is also too broad; define the viewing distance, lighting, location and whether a mark can be felt or seen in ordinary handling.
Select the sampling plan before seeing results
AQL is an acceptance-sampling framework, not a promise that the shipment’s defect rate is equal to or below the AQL and not a substitute for process control. It works only when the lot is defined, samples are selected without bias, categories are agreed in advance, and the proper table is used for the selected standard, inspection level, lot size and AQL. ISO 2859-1 specifies acceptance sampling for inspection by attributes; ANSI/ASQ Z1.4 is a widely used attributes-sampling standard.1 2
Use the current licensed copy of the chosen standard or a qualified inspection partner’s controlled tables to obtain the sample size, acceptance number (Ac) and rejection number (Re). Do not copy an unverified online chart into a purchase order. State whether the plan is normal, tightened or reduced inspection, whether it is single or another plan, and whether the lot is the full order, one production date, one SKU, or one carton-marking variant. A mixed lot can hide a variant-specific issue.
Separate defect severity from buyer preference
A disciplined classification prevents a cosmetic disagreement from becoming a shipment hold and prevents a genuine hazard from being negotiated away. Critical means a condition with an unacceptable safety, legal or serious-use risk. Major means the product is materially unfit for intended use, materially different from the approved specification, or likely to create a complaint or return. Minor means a visible but limited departure that does not materially impair normal use or saleability under the agreed standard.
A useful starting policy is zero acceptance for critical defects, with the exact Ac/Re plan explicitly written; stricter AQLs for major defects than minor defects; and a separate 100% check for properties that cannot be safely sampled. The values are commercial choices, not universal rules. In particular, a failed battery-compartment security check, wrong battery chemistry, exposed sharp edge, wrong product identity, or missing required warning should not be treated as a routine minor cosmetic count.
Use risk to decide where to spend inspection effort
Spend more effort on failure modes that are safety-relevant, difficult to detect after fulfillment, expensive to sort, or likely to affect many units. A lock switch that does not block erasure can destroy a child’s drawing or a retailer’s product experience. A mixed battery configuration can undermine product instructions and freight preparation. A weak master carton can turn otherwise conforming tablets into damaged inventory in transit. Conversely, a small molding witness mark on a hidden rear surface may be tolerable if it is consistent with the approved sample.
5. Inspection scope, quality and resource comparison
| Inspection approach | What it can establish | Resource impact | Best use | Key limitation |
|---|---|---|---|---|
| Document and carton-count review | Correct SKU, quantity, artwork revision, labels and packing list alignment | Low | Every shipment | Does not prove unit function |
| AQL-based final inspection | A statistically controlled view of agreed attribute defects in a defined lot | Moderate | Stable production with clear defect rules | Does not guarantee every unit is defect-free |
| 100% functional screening | Each unit receives specified functional checks | High | High-consequence function, rework campaign, new model or recurring defect | Still depends on test method and records |
| Packaging performance qualification | A packaging system’s performance under a defined laboratory procedure | Moderate to high | New carton, route, fulfillment method or damage history | Is not a substitute for final carton inspection |
| Laboratory compliance or reliability test | Evidence against a specified technical or regulatory requirement | Moderate to high | New market, modified design, safety-relevant change | A passing report does not confirm the packed lot matches the tested sample |
The right plan often combines these approaches. For example, inspect all master-carton markings and carton counts, sample finished units using a written attributes plan, run 100% checks where the factory can demonstrate automated functional screening, and retain the relevant laboratory or transport documents outside the inspection report. Packaging qualification should be selected for the actual distribution risk. ISTA 1A is an integrity test for individual packaged products of 68 kg or less, but ISTA cautions that its 1 Series tests are not simulations of actual transport hazards and may not cover conditions such as moisture or unusual handling.3
| Control area | Requirement to freeze | Evidence to capture at inspection |
|---|---|---|
| Product identity | Model, SKU, screen size, color, artwork revision, accessory set | Sample photos, SKU label, comparison to approved sample |
| Functional performance | Writing pattern, erase method, lock behavior, stylus retention, battery/charge behavior | Test record, defect photos or video, quantity tested |
| Appearance | Viewing condition, permitted molding marks, logo position, scratch and color standard | Reference photos, defect location and count |
| Battery and instructions | Chemistry, installed or packed-separately status, polarity marking, warnings and transport documents | Battery label photos, instruction revision, supporting documents |
| Packing | Inner quantity, dividers/protection, master-carton dimensions, gross weight, marks and seal method | Carton photos, count, measured dimensions and weight |
| Traceability | Lot/date/run code and factory/SKU mapping | Product and carton code photos, production summary |
6. Product and technical inspection detail
Verify identity, construction and cosmetic finish first
Start with product identity because a perfectly functional wrong SKU is still a major nonconformity. Compare the sampled tablet to the approved sample and controlled artwork for size class, exterior color, trim, logo, print language, button or switch placement, stylus color and accessories. Confirm that all supplied items are present and that no unapproved substitute has been introduced.
Inspect the front writing surface, bezel, back housing, corners, seams, fasteners, lock switch, erase button, stylus and any charging port. Use the pre-agreed lighting and viewing distance. Look for cracks, chips, burrs, deep scratches, stains, mismatched color, sink marks, excessive flash, loose parts, uneven printing, wrong logo orientation and gaps that exceed the approved sample. Note the location. A small mark on the rear differs commercially from a visible scratch across the writing area.
Do not classify all cosmetic variation as failure. Molded housings and liquid-crystal writing surfaces can show controlled variation. The buyer should define what normal variation is permitted by means of approved limit samples or high-resolution reference photographs. A defect is a departure from the agreed intended state with sufficient severity to impair foreseeable use; a nonconformity is a departure from a specification requirement.2 In practice, the written specification controls the release decision.
Test the writing surface as a writing surface
An LCD writing tablet is not necessarily a conventional LCD display. Do not inspect it with dead-pixel or brightness criteria unless the particular product actually has an illuminated pixel display. For the common pressure-responsive writing board, use the supplied stylus and make continuous strokes in the center, each quadrant, near the edge of the active area and, where appropriate, a small mark in the corners. Check that the line appears with the expected contrast, without unexplained blank zones, discontinuities or permanent marks that remain after the agreed erase test.
Test only the pressure range and environmental condition stated in the product specification. “Writes with very light pressure” should not be assumed for every model. If the buyer sells the product with a handwriting, note-taking or children’s drawing claim, the approved sample should define the expected visible result. Photograph abnormal areas beside a scale or identify them on a zone map. This allows the factory to distinguish a surface issue from a stylus issue during corrective action.
Verify erase and lock as a sequence, not as isolated button presses
For each sampled unit, write the agreed pattern, set the lock to the unlocked position, and activate erase once using the normal user control. The full pattern should clear in the manner defined by the approved reference. Then write a new pattern, set the lock to the locked position, attempt normal erase, and confirm that the writing remains. Return to unlocked and confirm that erase works again. Record any intermittent behavior, incomplete clearing, ghost image beyond the agreed limit, or lock position that is unclear, loose or reversed.
For a model with no lock, remove that test rather than marking it “not applicable” after the fact. For a model with a mechanical erase control, app control, multiple page memory or a rechargeable display, use the product-specific sequence. Never attempt a destructive reset, unauthorized disassembly or repeated cycling beyond the approved method during routine inspection. The objective is to verify finished-goods conformity, not to create an unrepresentative endurance test.
Check the stylus and accessory interface
A supplied stylus is part of the user experience and should receive its own acceptance criteria. Confirm the correct material, color, length and logo treatment where specified. Insert it into the holder or tether point repeatedly using normal force and check that it is retained during ordinary handling but can be removed without damage. Inspect for sharp molding flash, cracks, poor tether attachment or a holder so loose that the stylus falls out. If the stylus is packed separately, verify its quantity, bag, label and carton allocation.
Avoid blanket claims that a stylus is a safety device or that it will never be lost. The appropriate test depends on the product’s intended age grade and applicable requirements. If the tablet is a children’s product, the buyer should have the correct safety assessment and test program established before final inspection; the inspector should only verify that the released goods match the tested and approved configuration.
Verify the battery and power configuration without assumptions
First identify the agreed configuration: a replaceable coin/button cell, a sealed rechargeable cell, a replaceable cylindrical battery, or another design. Confirm that the unit, instructions, packaging and purchase order all describe the same configuration. Check accessible polarity marks where relevant, battery orientation, compartment closure, screw presence and engagement, battery contact condition, charge port condition and any indicator behavior stated in the specification.
For a tablet using replaceable button or coin batteries and intended for the U.S. market, CPSC’s guidance says the compartment must require a tool or two independent simultaneous hand movements to open and must not make the battery accessible or liberated in use-and-abuse testing. It also addresses product, packaging and instruction warnings under the applicable rule.4 A final inspection may verify the expected screw, compartment closure and warning placement, but it cannot replace the specified accessibility or abuse tests.
For rechargeable models, confirm the correct cable type and inclusion status, port fit, stated input labeling and the basic agreed charge/operation behavior. Do not call a product “UN 38.3 certified.” The relevant transport evidence is a battery test summary and classification/packing preparation, not a marketing badge. IATA says that, except for button cells installed in equipment, manufacturers and subsequent distributors of cells, batteries and battery-powered equipment manufactured after 30 June 2003 must make the UN Manual of Tests and Criteria 38.3 test summary available.5 Check the document against the battery model and transport plan, and have the freight forwarder determine the final shipment instructions.
Treat markings, manuals and traceability as product features
Inspect the product, retail package and carton for the approved model identifier, brand, destination-language instructions, battery warnings, age grading where applicable, barcode, country-of-origin statement where required, and legal or importer information specified by the buyer. Check scannability if barcodes are contractual. Verify that documents inside the retail box match the outer artwork revision.
Traceability is operationally valuable even where a buyer is not using a particular regulatory scheme. It allows a defect to be linked to a production run, component change or carton range. EU guidance states that manufacturers must meet applicable traceability requirements, including product type, batch or serial identification and manufacturer contact details, and that importers must verify these elements before market placement.6 For U.S. children’s products, CPSC guidance describes visible, legible, permanently affixed tracking marks with manufacturer/importer, production location and date, and batch or other source-identifying information, to the extent practicable.9
7. Sample, testing and quality-control workflow
Build the inspection pack before the inspection date
Send the inspector a controlled inspection pack at least several working days before inspection. It should contain the purchase order; approved sample photos; bill of materials or key-component list; functional test sequence; defect definitions with photo examples; AQL plan; artwork files; inner and master-carton specifications; barcode list; packing list; destination requirements; and a report template. State the inspection date only after production is complete enough that units are finished and the agreed proportion of goods is packed.
Ask the factory for a production and packing summary by SKU, color and carton. Reconcile this total to the lot definition. The inspector should select cartons across the warehouse without factory preselection, then draw units across cartons, colors and shifts where those are within scope. Record the sampled-carton numbers; otherwise, a retest cannot demonstrate whether a corrected population was actually resampled.
Follow a repeatable inspection sequence
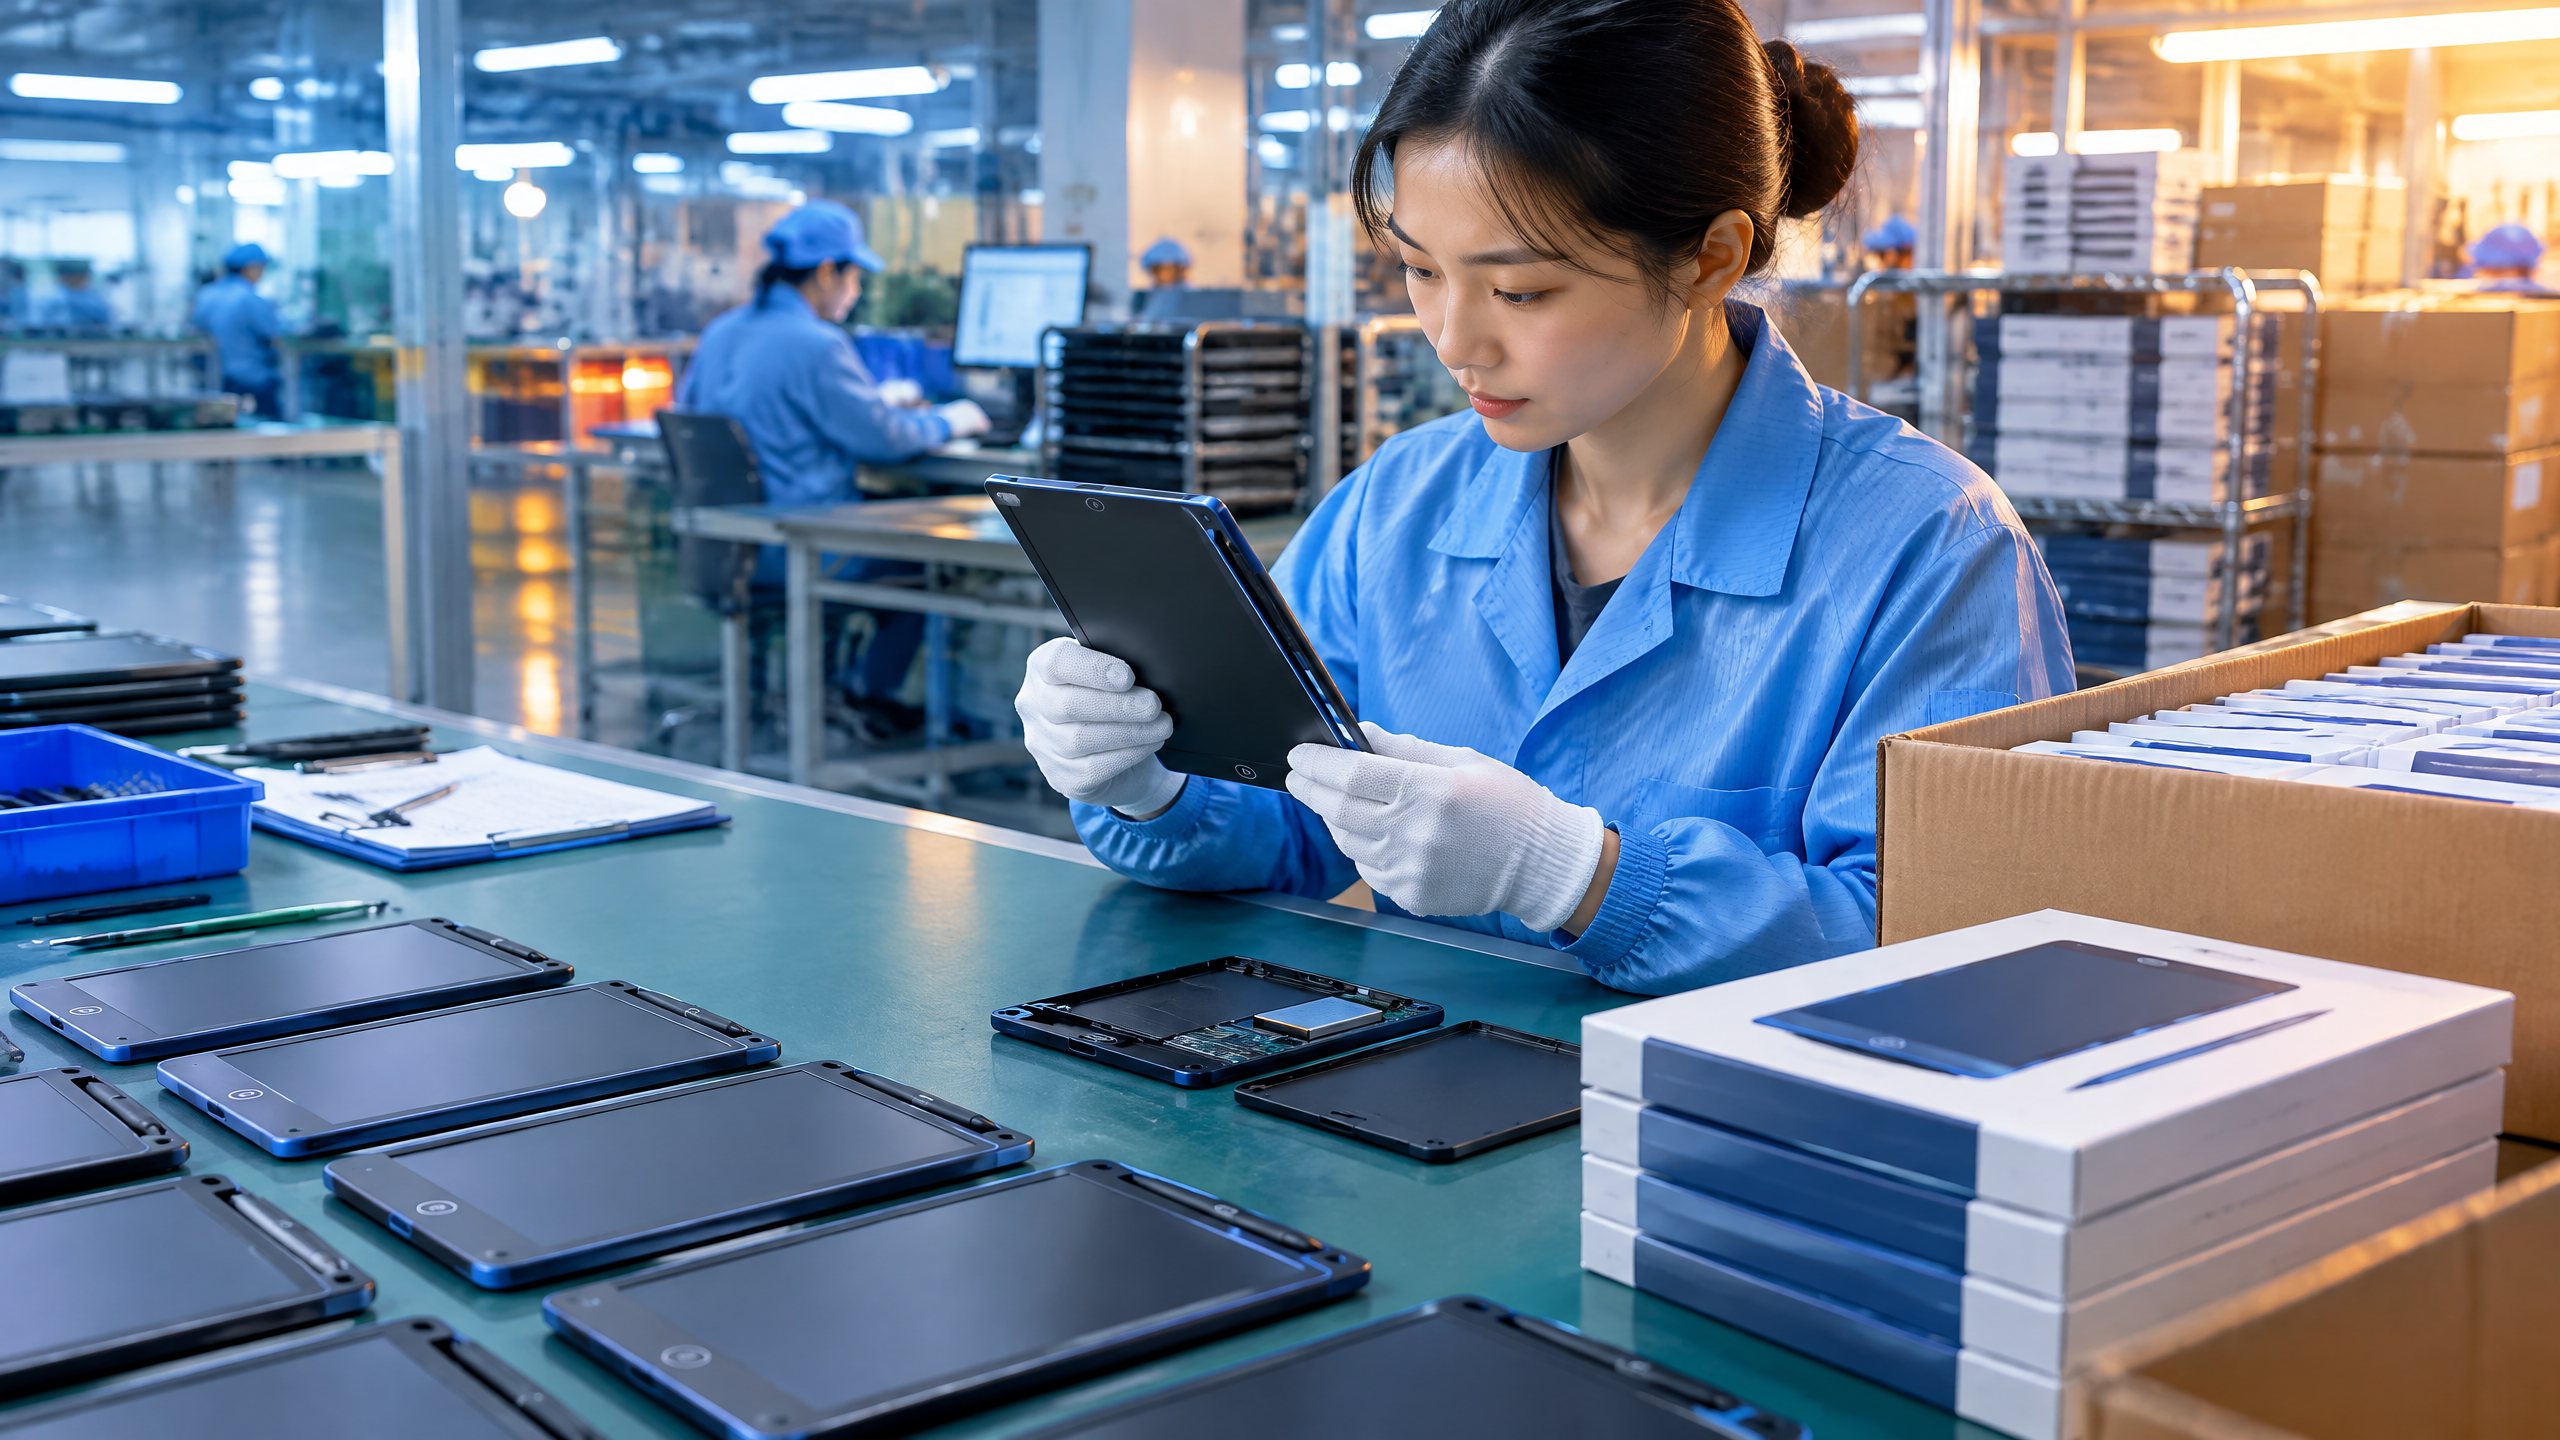
Begin with an opening meeting to reconfirm model, lot size, packed percentage and safety holds. Count master cartons, compare carton marks to the packing list, and select the sample. Then inspect unit identity and cosmetics, execute functional tests, check accessories, inspect battery/power configuration, review marking and documentation, and examine inner and outer packaging. Measure only dimensions and weights that are contractual or operationally important, using calibrated or verified tools.
Keep the sampling hierarchy clear. Use an AQL attributes plan for discrete results such as “lock fails” or “logo reversed.” Use variables controls for dimensions or weight where the specification has a tolerance and the buyer has selected a variables plan or 100% measurement. Do not convert a vague observation into a defect count merely to fill an AQL form. If a requirement has no limit, decide it with the buyer before release.
A concise functional routine for each selected standard model can be:
- Verify model, color, logo, accessories and visible condition against the approved reference.
- Create the defined writing pattern with the supplied stylus across the active area.
- Erase with lock off and inspect the result under the agreed viewing condition.
- Write again, engage lock, attempt erase, then unlock and confirm normal erase returns.
- Check stylus fit or tether, battery compartment/charging interface, instructions and required markings.
- Return the unit to its original pack or clearly quarantine it if it has been damaged, opened beyond normal inspection, or identified as defective.
This list is a functional-screening protocol, not a battery life, drop, temperature, ingress or endurance claim. If repeated erase cycles or environmental performance are product requirements, define a separate reliability plan with cycle counts, conditioning and pass/fail limits before testing.
Record, classify, verify and decide
Each defect record should include a unique number, SKU, carton identifier, sample number, defect category, severity, clear description, location, photo and the requirement it violates. Photographs should show both context and close-up detail. A defect rate without evidence is difficult to correct; a photo without the relevant specification is difficult to classify consistently.
Compare the final validated count for each severity against the agreed Ac/Re criteria. Separately list any shipment-stopping condition such as a critical defect, wrong SKU, missing required documentation, carton count discrepancy, wrong artwork revision, missing battery warning, mixed battery configuration or unresolved security issue. Do not allow a total minor count to cancel a major failure, or a good AQL result to override a hold condition.
If the lot fails, issue a nonconformance report and require a written corrective-action and sorting plan that identifies the affected population. A credible re-inspection follows completed rework or sorting and uses a newly selected sample. Re-inspecting only the factory’s repaired showcase units is not evidence that the lot has been corrected. When defect patterns suggest a systematic issue, the buyer may require 100% sorting, a new production lot, further testing, a commercial remedy, or cancellation according to the contract.
8. Ordering and implementation preparation
Put the release rules in the purchase order
The purchase order or quality agreement should state the product revision, approved sample identifier, lot definition, inspection standard/version, inspection level, AQL or Ac/Re thresholds by severity, critical-defect policy, required functional tests, packaging specification, report timing, re-inspection process, release authority and payment/freight hold. It should also define who pays for the first and repeat inspections and who may authorize deviations.
A statement such as “AQL 2.5” is incomplete. It does not specify whether it applies to major or minor defects, which standard table and inspection level are used, how critical defects are treated, or what happens if the lot includes several SKUs. A compact quality annex is usually clearer than trying to resolve these details by email during inspection.
Lock change control and records
Require the factory to notify the buyer before changing a battery supplier, cell model, housing resin, stylus, screen supplier, printed artwork, packaging material, firmware, charging component or assembly location. A component or marking change can affect appearance, function, tested configuration, freight preparation or legal documentation. The buyer should decide whether a revised approved sample, targeted test or new inspection criteria are needed.
Keep the signed sample record, final inspection report, photos, packing list, corrective-action records, shipping marks, applicable test reports and transport documents together by purchase order and lot. Retention should follow the applicable law, contract and market requirements. In the EU, for products requiring CE marking, the manufacturer must retain the declaration of conformity and supporting technical documentation for at least 10 years after placement on the market.7 That legal retention rule is not a generic rule for all tablets, but it illustrates why version-controlled records matter.
Keep QC distinct from market access and freight release
A passed factory inspection is not permission to apply a CE mark, an FCC authorization or a safety claim. If a tablet includes radio functions, the FCC states that RF devices subject to equipment authorization must meet applicable technical requirements before U.S. marketing or importation, with the required approval procedure, testing, labeling and records.10 For the EU, CE marking applies only where harmonised EU rules require it, and the responsible manufacturer must identify applicable requirements, complete conformity assessment, assemble evidence and sign the declaration of conformity before affixing it.7
Treat the final release as a gated decision: quality evidence, packing evidence, document check and freight readiness must all be satisfactory. The buyer, not the inspector, owns the commercial decision to release payment or booking unless the contract explicitly delegates that authority.
9. Practical applications and scenarios
Scenario: promotional distributor with a logo-sensitive order
A distributor orders a standard non-rechargeable tablet with a printed logo for a campaign. The highest practical risks are the wrong logo artwork, inconsistent print position, wrong housing color, missing stylus and a lock that fails during normal use. The checklist should put identity and logo comparison before broad cosmetic sampling, apply the agreed major/minor thresholds, and require carton labels that distinguish the campaign SKU from similar stock. An immaculate generic tablet with the wrong logo is a major identity failure.
Scenario: education supplier with a coin-cell model
An education supplier intends to sell a tablet that uses a replaceable coin cell. The inspection verifies the exact tested battery configuration, compartment screw or intended opening mechanism, warnings and instruction revision, as well as erase, lock and stylus performance. The buyer separately confirms applicable age grading, laboratory testing, certification and tracking-label obligations. The pre-shipment report should never state that an inspector’s visual screw check proves product compliance or child resistance.
Scenario: retailer shipping through a parcel network
A retailer expects individual retail packages to move through a fulfillment center and parcel carrier. The final inspection checks retail-box condition, protective inserts, barcode, inner-pack quantity and master-carton strength/closure against the approved packing specification. If the route or packaging is new, the buyer may arrange a separate packaging qualification. ISTA notes that the shipper must define product damage, permitted tolerance and the method for assessing product and package condition after testing.3 This prevents a packaging test from being judged by an invented standard after damage occurs.
Scenario: rechargeable, wireless tablet variant
A premium variant has a rechargeable battery and radio function. The functional checklist expands to include the agreed charging behavior, port/cable configuration, radio-function basics and software or pairing version where applicable. It also holds the batch until the correct regulatory and transport evidence is available. The buyer must make sure that the packed configuration remains the one evaluated for market access; a late battery or firmware change is a change-control event, not a cosmetic substitution.
10. Detailed FAQ
What is the difference between an AQL inspection and a 100% inspection?
An AQL inspection selects a sample from a defined lot and uses a predetermined acceptance-sampling plan to decide whether the lot meets the agreed acceptance criteria. A 100% inspection applies a stated check to every unit. AQL is normally more efficient for stable production, while 100% screening may be appropriate for a high-risk function, a new design, a known recurring problem or a corrective-action sort. Neither method is meaningful without an unambiguous pass/fail test and records.
Is AQL 2.5 the correct standard for every LCD writing tablet order?
No. There is no universal AQL value for this product category. AQL values and inspection levels should reflect the consequence of failure, product price, destination, customer promise, history of the supplier and feasibility of screening. Critical conditions should have an explicit zero-acceptance policy or other written Ac/Re rule. Major and minor thresholds should be separate. The sampling table must match the chosen standard, lot size and inspection setting.
Should a failed erase function be critical or major?
For a normal LCD writing tablet, a unit that cannot erase when unlocked is generally a major functional defect because the product cannot deliver its central intended use. It can be escalated if the buyer’s specification or use case makes the failure safety-relevant or legally significant. A malfunctioning lock is typically major because it defeats an advertised or expected user control. The quality agreement, not an informal industry label, should make the final classification clear.
How should ghosting or residual marks after erase be judged?
Judge it against a pre-agreed, observable standard. The approved sample, viewing condition, background color and writing pattern should establish what residual image is acceptable. If the buyer requires no visible residual marks, write that requirement explicitly. If limited ghosting is inherent in the approved product, document the allowed level with photo limit samples. Do not create a new aesthetic threshold at the inspection table.
Do we need to test every stylus and tablet holder?
That depends on risk and order design. At minimum, include stylus presence, correct type and holder/tether fit in the agreed sample inspection. Consider 100% confirmation if stylus omission or poor retention has occurred before, if the tablet is sold as a complete ready-to-use kit, or if the packing process is manual and the accessory is easily missed. The test should use normal insertion/removal rather than arbitrary force unless a force requirement has been validated.
What battery checks belong in final inspection?
Confirm the agreed battery type and model, installed or separately packed status, orientation/polarity marks where relevant, compartment closure, screws, accessible contacts, warning and instruction revision, and charger/cable configuration for rechargeable products. For lithium-based batteries, verify that the applicable transport documents and test summary align with the actual battery model and transport plan. Final inspection does not replace mandated accessibility, abuse, electrical-safety or transport testing.
Can an inspector verify CE, FCC or children’s-product compliance during a pre-shipment inspection?
An inspector can verify that labels, documents and the packed configuration match the buyer’s approved files. That is valuable, but it is not the same as determining legal compliance. Regulatory status depends on applicable rules, product functions, records, test results and responsible economic operators. A private-label buyer selling under its own brand may be considered the manufacturer in the EU framework and carries the related responsibilities.7 Obtain market-specific advice and testing before shipment release, not after inventory reaches a fulfillment center.
What carton checks matter most for LCD writing tablets?
Check master-carton quantity, SKU and revision mark, gross weight, dimensions, product orientation, barcode or shipping mark, seal method, carton integrity, moisture or crush damage, inner-pack quantity, dividers or protection, and a representative carton’s actual contents. Also confirm that cartons do not mix colors, battery configurations or artwork revisions unless the packing list permits it. For air shipments with regulated batteries, coordinate final marks, quantities and documents with the freight forwarder.
What should happen when an inspection fails?
The buyer should place the lot on hold, receive the full defect evidence and factory root-cause/corrective-action plan, and decide whether to rework, sort, replace, downgrade, retest or cancel under the contract. Any re-inspection should be scheduled only after corrective action is complete, with a fresh random sample and an updated report. Shipment release should not be based on a verbal assurance that the issue was fixed.
11. Conclusion and final email-only CTA
A useful LCD writing tablet pre-shipment inspection checklist does not merely list “appearance” and “function.” It ties a controlled product reference to a defined lot, a valid sampling plan, practical erase/lock/stylus/battery checks, clear cosmetic boundaries, carton evidence, traceability and a documented release gate. Its real value is early decision-making: the buyer can accept a conforming lot, hold a nonconforming lot, or require targeted correction while the goods are still under the supplier’s control.
For LCD writing tablets, talking flashcard machines and smart electronic badges, LcdWritingTablet can help translate an approved configuration into a model-specific pre-shipment inspection checklist. To discuss your product and quality requirements, email info@lcdwritingtablet.com.
References
Turn this sourcing plan into a product brief.
Share your target market, product requirements, packaging preference and estimated volume for a practical OEM / ODM discussion.